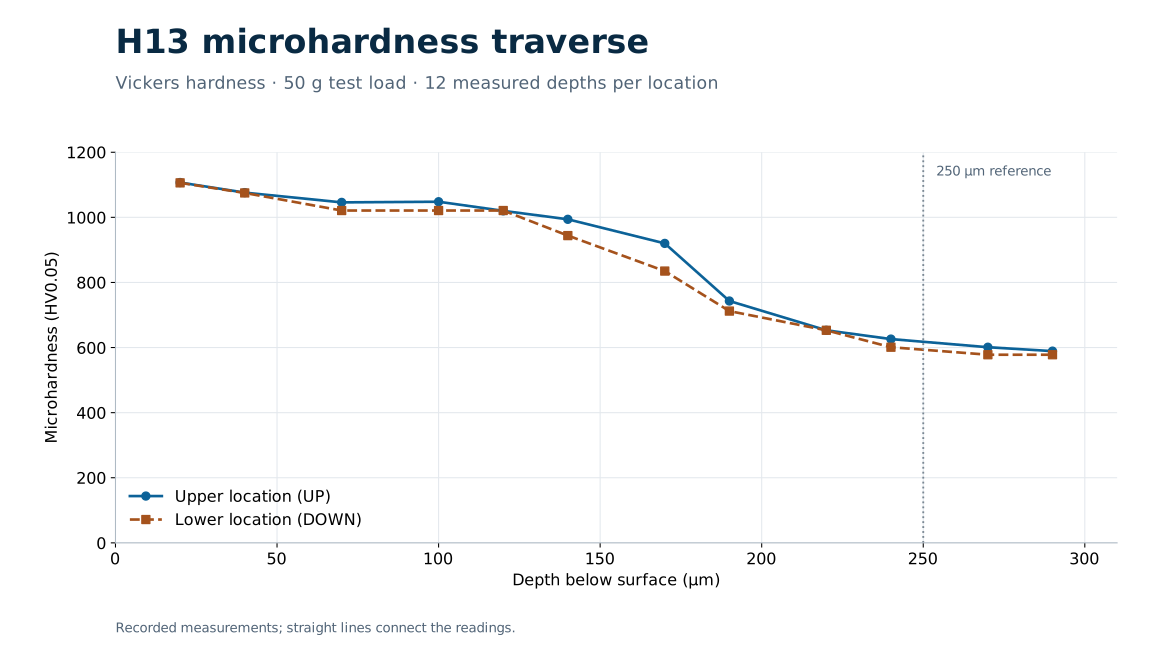
H13 plasma nitriding: case depth and hardness
Review the micrographs and 24-point microhardness traverse from the published technical case study.
ExplorePatt Technologies · Quebec, Canada
Wire electrical discharge machining for precision profiles, openings and hardened tooling. Review workpiece dimensions, thickness and critical geometry with Patt.

Profiles, slots, apertures and screen-support features in electrically conductive materials. Wire EDM is especially useful when mechanical tool access is limited or a component is already hardened.
| Parameter | Capacity |
|---|---|
| Machine travel | 800 × 600 × 505 mm31.5 × 23.62 × 19.88 in |
| Maximum workpiece | 1,250 × 1,020 × 505 mm49.21 × 40.16 × 19.88 in |
| Maximum load | 3,000 kg6,614 lb |
Why Patt
We work with tool steels, stainless steels and difficult alloys used in extrusion tooling and industrial machinery. Identify the grade, heat-treated condition, critical tolerances and inspection requirements when sending your drawing.
Our own polymer-processing equipment gives our machining team direct experience with wear, corrosion, sealing surfaces and service repair. We apply that experience to industrial customer parts.
Our process
Review the polymer or part, operating conditions, drawings and production targets.
Coordinate flow geometry, material, surface treatment and the installation envelope.
Bring machining, nitriding and dimensional checks together in our Quebec facility.
Discuss installation, operation, cleaning and ongoing service with the team who built it.
Patt Technologies
Review the micrographs and 24-point microhardness traverse from the published technical case study.
Explore
See the geometry, installation envelope and material options behind the Patt wave upgrade.
ExploreDiscuss your project
Send the polymer, throughput and operating conditions, or the drawing and material requirements for your part.
sales@patt-tech.com