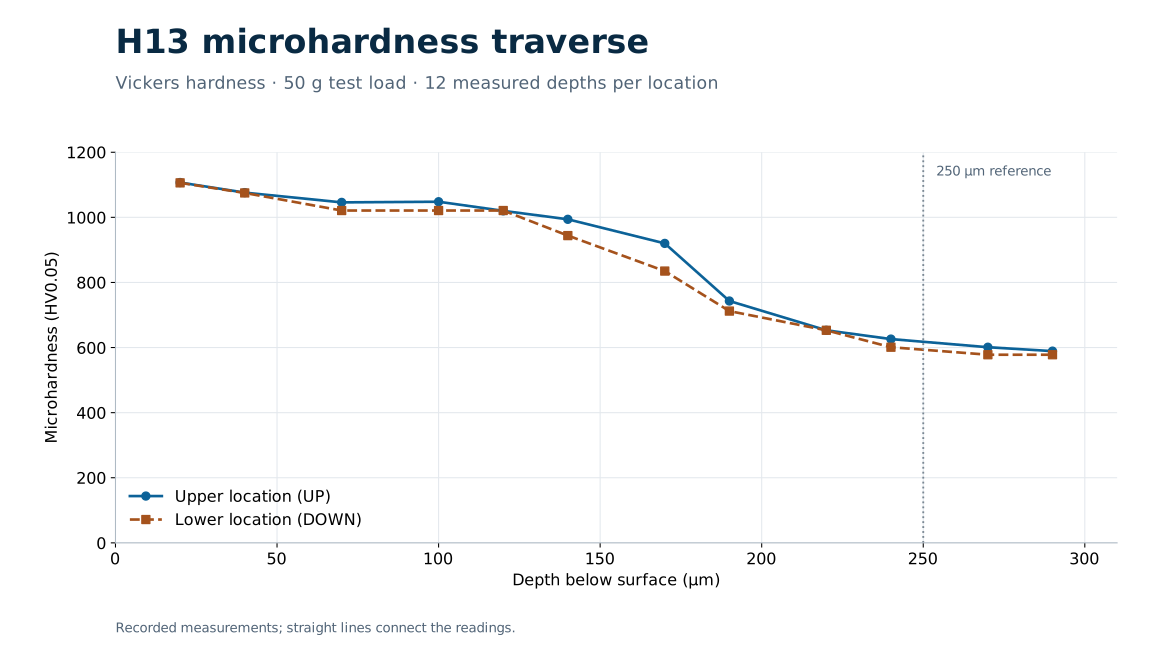
H13 plasma nitriding: case depth and hardness
Review the micrographs and 24-point microhardness traverse from the published technical case study.
ExploreQuebec engineering · Global service
Patt was founded in 1986 to solve real plastic-extrusion filtration problems. In-house machining and plasma nitriding grew from the same need to control reliability, wear and precision.
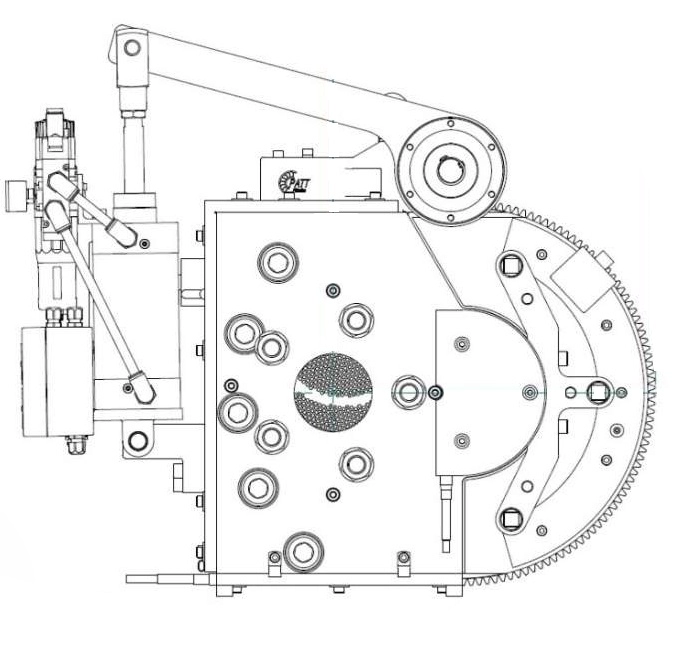
An integrated manufacturer
Designing filtration equipment for actual production made machining, material selection, heat treatment, surface engineering, controls and field service inseparable disciplines at Patt.
That integrated experience is also available to outside machining and nitriding customers—not only for Patt equipment.
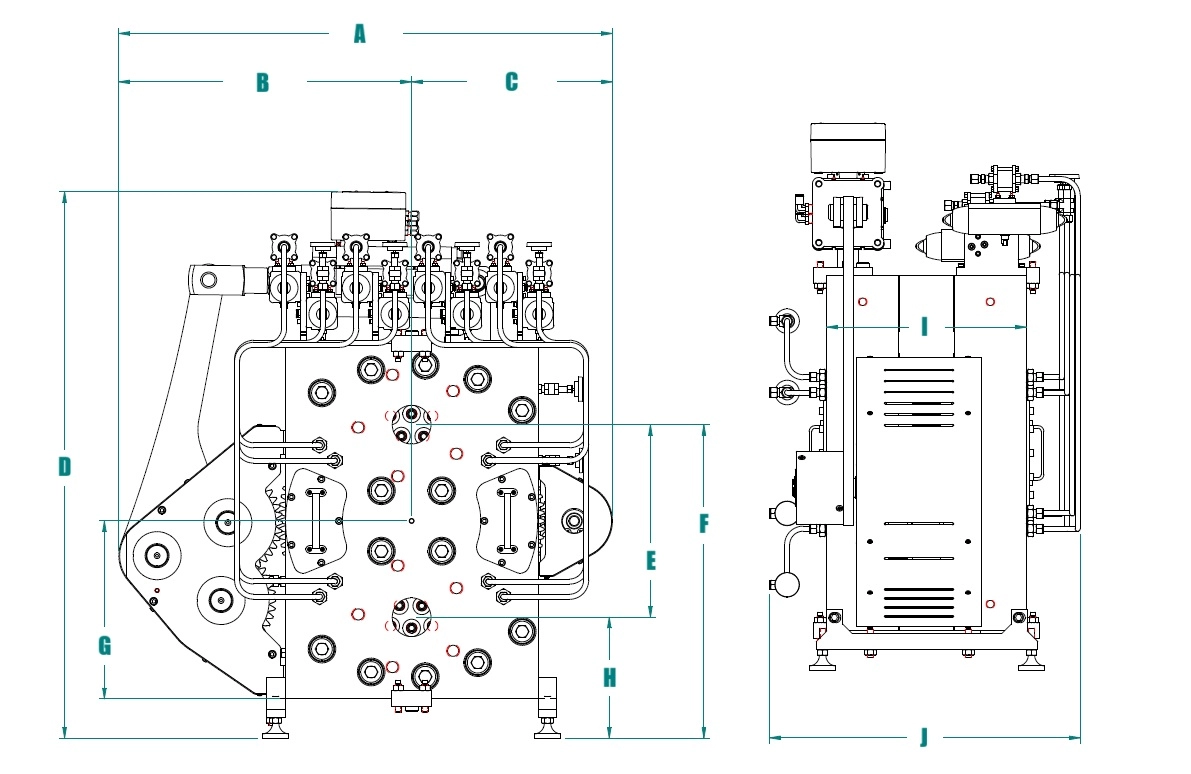
Saint-Eustache, Quebec facility · 588 Boulevard Industriel
Operating engineering, heavy machining, tooling-steel development and pulse plasma ion nitriding in a single plant eliminates subcontracting handoffs between machine shops and commercial heat treaters. Every tolerance stack, stock allowance, stress-relief step and nitrided case is controlled as one manufacturing sequence.
| Discipline | In-house equipment & documented envelope | Industrial deliverables |
|---|---|---|
| Continuous melt filtration systems | Constant-pressure rotary disk platforms (Rotary III sizes A–G: 10–1,990 cm²; Rotary IV monoblock sizes A–D: 10–385 cm²) and Colossus modular candle filters (1,385–7,000 cm² per unit), rated up to 450 °C and 5,800–6,500 psi. | Complete filtration systems, Rotary Control PLC drives, 1.8× wave-shaped breaker plates, laser-cut screen packs and melt pressure sensors. |
| Proprietary tooling steels | Five engineered plastics-tooling grades benchmarked against AISI H13 across seven design criteria: PEA (48–49.5 HRC), Structural (51.5–53.3 HRC), PEA+ (47.5–50.5 HRC), Patt Tool (50–57 HRC) and Patt Corrosion (42–48 HRC). | Finish-machined and nitrided filter housings, rotary disks, strand dies, breaker plates, wear sleeves and corrosive-polymer melt components. |
| Pulse plasma / ion nitriding (since 1992) | Industrial pulsed DC glow-discharge furnace with a 1,200 × 1,200 mm (120 × 120 cm) useful chamber and 2,000 kg (2 metric tons) load capacity, operating at 350–540 °C in high-purity N₂/H₂ vacuum atmospheres. | Conventional diffusion cases (250 µm+ on H13), low-temperature stainless S-phase / expanded martensite and engineered γ′ / ε compound layers for Patt and outside customer parts. |
| Heavy precision machining & extrusion tooling | Surface grinding up to 1,500 × 1,000 × 900 mm (3,000 kg), wire EDM up to 1,250 × 1,020 × 505 mm workpiece (3,000 kg), 3- and 4-axis CNC milling up to 940 × 940 × 1,000 mm (1,500 kg), and turning up to 670 mm swing × 2,000 mm. | Custom strand dies, extruder-to-filter adapters, flanges, heated crossover pipes, precision ground plates and contract machining for North American industry. |
Patt’s technical publications document measurable engineering gains rather than generic marketing claims. In polymer filtration, Patt’s wave-shaped breaker plate upgrade—featured in Canadian Plastics—delivers 1.8× active filtration screen area within the same nominal breaker-plate diameter while adding only approximately 15 mm of axial housing width, reducing pressure drop and extending screen life on existing and new extrusion lines.
In surface engineering, Patt’s H13 pulse plasma nitriding case study publishes original cross-sectional optical micrographs alongside 24 microhardness traverse readings (HV0.05) from 20 µm to 290 µm depth across upper and lower part locations, documenting surface hardness above 1,100 HV0.05 and effective diffusion cases exceeding 250 µm. Every production project is supported by in-house coordinate measuring (CMM), optical inspection, surface-finish verification and macro/micro-hardness testing.
Yes. In addition to manufacturing Patt filtration systems and extrusion tooling, our Saint-Eustache facility provides contract large-part surface grinding, wire EDM, CNC machining and pulse plasma (ion) nitriding for outside manufacturers across Quebec, Ontario, Canada and the United States. Customers can supply finished or semi-finished components for ion nitriding in our 1,200 × 1,200 mm (2,000 kg) furnace, or send 2D/3D CAD drawings for turnkey machining and surface hardening.
High-pressure polymer filtration disks, strand dies and breaker plates depend on the interaction between core yield strength, flatness/parallelism and nitrided case architecture. Managing alloy selection (PEA, Structural, PEA+, Patt Tool, Patt Corrosion or H13/stainless), pre-finish grinding allowances and low-distortion pulse plasma nitriding under one roof eliminates inter-vendor tolerance disputes and prevents white-layer spalling or sealing-face leakage.
Patt supports polymer processors and industrial OEMs across Canada, the United States, Europe and international markets in English, French, German, Spanish and Chinese. Our engineering team accepts PDF, DWG, DXF, STEP, IGES, JPG, PNG and ZIP packages directly through our online RFQ portal or via sales@patt-tech.com, with direct phone access to our main plant (+1-450-473-4888) and engineering/sales desk (+1-450-689-2497).
Patt Technologies
Review the micrographs and 24-point microhardness traverse from the published technical case study.
Explore
See the geometry, installation envelope and material options behind the Patt wave upgrade.
ExploreDiscuss your project
Send the polymer, throughput and operating conditions, or the drawing and material requirements for your part.
sales@patt-tech.com