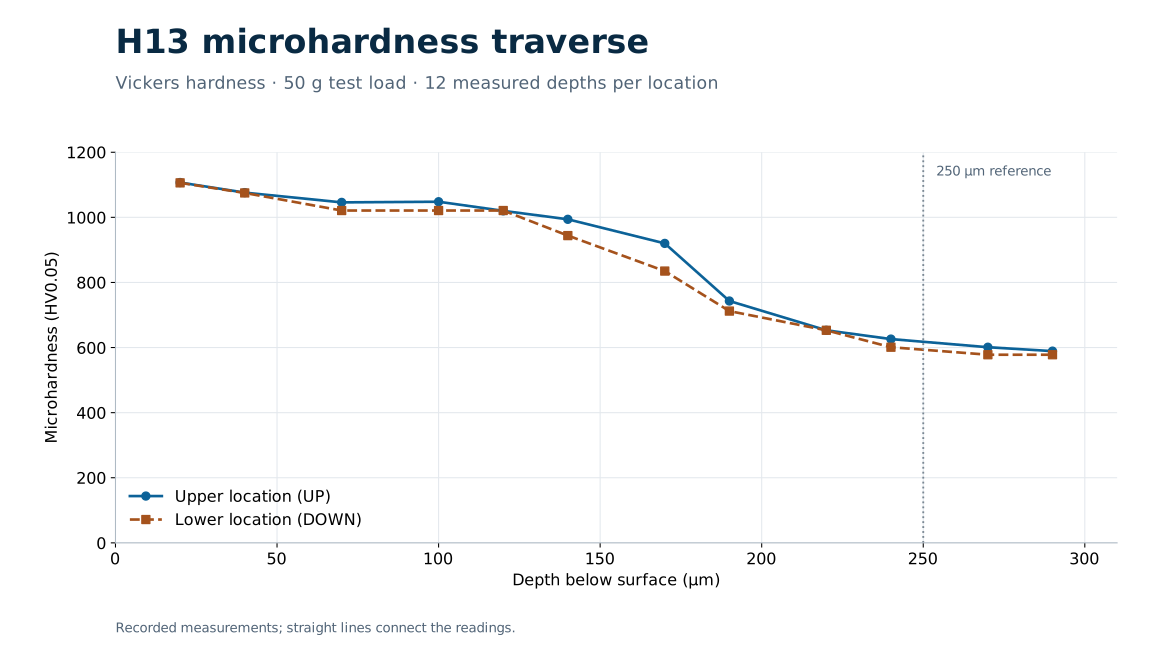
H13 plasma nitriding: case depth and hardness
Review the micrographs and 24-point microhardness traverse from the published technical case study.
ExplorePatt steels · Plastics tooling
Five Patt grades for different balances of core strength, wear, corrosion and surface finish. Choose the material around your resin, operating temperature and tooling requirements.
Engineering reference
Choose corrosion-resistant extrusion tool steels and stainless mould steels by the failure mechanism you need to solve. Start with the existing grade and service conditions, then compare Patt’s alloy and surface-treatment options.
| Starting material | When you observe / require | Patt candidate | Engineering selection check |
|---|---|---|---|
| H13 / 1.2344 hot-work steel | Pitting or corrosion in an aggressive polymer service | PEA or Patt Corrosion | Prioritize the actual corrosion mechanism, then check core strength, toughness and treatment. |
| H13 / 1.2344 hot-work steel | Core loading or surface indentation limits the tool | Structural, with a suitable surface-treatment review | Confirm section size, heat treatment, stress and required case support. |
| 420-family stainless mould steel / 1.2083 | Corrosion resistance is needed together with a different strength / toughness balance | PEA or PEA+ | Compare certified hardness, polish requirements and corrosion performance in the formulation. |
| D2 / 1.2379 cold-work steel | Abrasive wear, chipping or elevated-temperature service calls for a different balance | Patt Tool | Review wear mode, toughness and service temperature; hardness alone does not predict life. |
| 4140 / 42CrMo4-family engineering steel | A strong support component now needs better melt-contact wear or corrosion performance | Structural or PEA | Separate structural load requirements from working-surface corrosion and wear requirements. |
| Polished stainless flow-channel tooling | Surface finish must be retained under combined wear and corrosion | PEA+ or PEA | Review polish, resin chemistry, nitriding response and final dimensional requirements. |
This is a selection matrix, not a certified grade-equivalence or automatic substitution list. Standard designations identify material families; verify the supplied specification and certificate. Stavax ESR is a branded modified 420-family grade. Patt candidates must be selected against the actual duty and the published grade data below.
Explore PEA, PEA+, Structural, Patt Tool and Patt Corrosion.
Engineering selection scores: 0–100 in steps of 5. Mechanical ranges include program results and engineering estimates.
Balanced extrusion tooling
PEA balances core strength, corrosion resistance and a fine working finish for extrusion tooling. Its precipitation-hardened stainless core supports dies, breaker plates, filter bodies and precision melt-contact components. Plasma nitriding adds a hard working surface for sliding and polymer-contact wear.
| Mechanical property | Design values |
|---|---|
| Core hardness | 48–49.5 HRC |
| Tensile strength | 1,700–1,900 MPa246.6–275.6 ksi |
| Charpy V-notch impact | 44 J32.5 ft·lb |
Core strength and load support
Structural prioritizes core strength and load support in highly stressed tooling. Its high aged hardness supports resistance to indentation and permanent deformation, including beneath a nitrided case. Typical applications include loaded breaker plates, support components, inserts and wear parts.
| Mechanical property | Design values |
|---|---|
| Core hardness | 51.5–53.3 HRC |
| Tensile strength | 1,780–1,950 MPa258.2–282.8 ksi |
| Charpy V-notch impact | 35–80 J25.8–59 ft·lb |
Corrosion and toughness
PEA+ combines a refined precipitation-hardening system with a fine, polishable matrix. It targets a balanced combination of strength, toughness and corrosion resistance for precision dies, polished flow channels and demanding melt-contact tooling.
| Mechanical property | Design values |
|---|---|
| Core hardness | 47.5–50.5 HRC |
| Tensile strength | 1,660–1,850 MPa240.8–268.3 ksi |
| Charpy V-notch impact | 45–90 J33.2–66.4 ft·lb |
Wear and elevated-temperature tooling
Patt Tool is designed for elevated-temperature plastics tooling and abrasive service. A carbide-bearing core combines high working hardness with temper resistance, supporting wear inserts, filled-compound tooling and high-temperature extrusion components. Its material-selection profile places temper resistance above H13 with comparable abrasive wear resistance.
| Mechanical property | Design values |
|---|---|
| Core hardness | 50–57 HRC |
| Tensile strength | 1,750–2,070 MPa253.8–300.2 ksi |
| Charpy V-notch impact | 6–25 J4.4–18.4 ft·lb |
Corrosion-focused tooling
Patt Corrosion prioritizes corrosion resistance for melt passages, dies and precision tooling exposed to aggressive processing residues and cleaning environments. Its lower working-hardness range supports a toughness-focused balance for components where corrosion is the principal material-selection driver.
| Mechanical property | Design values |
|---|---|
| Core hardness | 42–48 HRC |
| Tensile strength | 1,420–1,680 MPa206–243.7 ksi |
| Charpy V-notch impact | 80–170 J59–125.4 ft·lb |
While AISI H13 offers high temper resistance (score 90/100), its corrosion resistance is low (score 10/100) when exposed to PVC, CPVC, halogenated flame retardants, acidic recycled-polymer condensates or hydrolysis cleaning. PEA (corrosion 80/100), PEA+ (corrosion 85/100, polishability 95/100) and Patt Corrosion (corrosion 95/100) provide stainless corrosion protection alongside high core strength and toughness.
For high axial melt pressure and bending loads—such as large wave-shaped breaker plates and filter housings—Structural delivers the highest core load capacity (score 90/100, 51.5–53.3 HRC, 1,780–1,950 MPa tensile strength). For elevated-temperature abrasive compounds with glass or mineral fillers, Patt Tool offers 50–57 HRC hardness and 95/100 temper resistance.
Yes. All five Patt grades are engineered to work with Patt’s in-house pulse plasma ion nitriding processes—including low-temperature stainless routes that harden the wear surface against sliding and scraper damage while preserving the core hardness and corrosion behaviour of the alloy.
Patt Technologies
Review the micrographs and 24-point microhardness traverse from the published technical case study.
Explore
See the geometry, installation envelope and material options behind the Patt wave upgrade.
ExploreDiscuss your project
Send the polymer, throughput and operating conditions, or the drawing and material requirements for your part.
sales@patt-tech.com