Strand dies & die components
Strand pelletizing dies, die bodies, orifice plates, die lips and internal melt-distribution manifolds machined, ground and polished for uniform flow balance and clean strand discharge.
Request a die quotePolymer Melt Transfer Tooling · Since 1986
Custom extrusion tooling from the extruder outlet to the die: strand dies, adapters, breaker plates, crossover pipes and elbows. Coordinate the flow geometry, steel and surface treatment with one manufacturing team.

Melt-path components
Every transition between the extruder barrel, melt pump, screen changer and die affects residence time, pressure drop, sealing integrity and cleaning downtime. Patt machines both new custom assemblies and retrofit transition pieces to match existing line centrelines.
Strand pelletizing dies, die bodies, orifice plates, die lips and internal melt-distribution manifolds machined, ground and polished for uniform flow balance and clean strand discharge.
Request a die quoteCustom transition adapters, C-clamp flanges, split rings and bolted spools connecting extruders, melt filters, gear pumps and dies with coordinated bore transitions and high-pressure sealing faces.
Request an adapter quoteMelt-transfer pipework and angled elbows built around plant layout, connection orientation, heater-band zoning, melt-pressure sensor ports and streamlined internal transitions that avoid dead spots.
Discuss melt pipeworkThis stainless-steel strand die illustrates Patt’s integrated workflow: CNC machining and precision grinding of internal flow passages and mating faces, followed by low-temperature pulse plasma (ion) nitriding to protect the die face and strand orifices against cleaning-tool damage, abrasion and polymer corrosion.

Scroll horizontally to compare all columns.
| Component family | Engineering, machining and surface-treatment focus | Typical materials & treatments |
|---|---|---|
| Strand dies and die assemblies | Internal melt-distribution channels, transition geometry, strand-hole arrays, die faces and precision ground sealing surfaces designed for low hang-up and repeatable cleaning. | Patt PEA, PEA+, Patt Corrosion, H13, 420 / 17-4PH / 316L stainless + pulse plasma / ion nitriding |
| Extruder-to-filter & filter-to-die adapters | Bore diameter transitions (circular-to-circular or circular-to-slot), high-pressure metal-to-metal sealing faces, bolt circles, alignment dowels and standard ½-20 UNF melt-sensor / thermocouple ports. | Patt Structural, PEA, H13, 4140 / 4340, precipitation-hardening stainless steels |
| Heated crossover pipes & elbows | Custom centreline offsets, multi-axis melt-transfer routing, matched heating zones, smooth internal transitions and disassembly access for pyrolysis or mechanical cleaning. | Patt PEA, Patt Corrosion, H13, nitriding steels and corrosion-resistant alloys |
| Flat & wave-shaped breaker plates | Precision-drilled and wire-EDM flow passages and screen-support ribs, including Patt’s wave-shaped breaker plate upgrade delivering 1.8× active screen area in approximately +15 mm width. | H13, Dievar, Patt Tool, Patt Structural + conventional or low-temperature ion nitriding |
Single-source accountability
Extrusion dies and adapters frequently fail at the intersection of base-metal strength, thermal distortion and surface wear or acid corrosion from PVC, CPVC, flame-retardant compounds and post-consumer recycled (PCR) resins. Producing the component in one facility allows Patt to coordinate stock allowances, stress relief, finish grinding and surface hardening as a single engineered sequence.

Documented equipment envelope
Scroll horizontally to compare all columns.
| Process | Machine / chamber envelope | Maximum workpiece | Maximum weight |
|---|---|---|---|
| Precision surface grinding | 1,500 × 1,000 × 900 mm59.06 × 39.37 × 35.43 in | Drawing review required | 3,000 kg6,614 lb |
| Wire EDM | 800 × 600 × 505 mm31.5 × 23.62 × 19.88 in | 1,250 × 1,020 × 505 mm49.21 × 40.16 × 19.88 in | 3,000 kg6,614 lb |
| CNC milling | 840 × 840 × 760 mm33.07 × 33.07 × 29.92 in | 940 × 940 × 1,000 mm37.01 × 37.01 × 39.37 in | 1,500 kg3,307 lb |
| CNC & centre turning | 670 mm swing26.38 in swing | 2,000 mm between centres78.74 in between centres | Drawing review required |
| Pulse plasma / ion nitriding | 1,200 × 1,200 mm (120 × 120 cm)47.24 × 47.24 in (120 × 120 cm) | Geometry & fixture review | 2,000 kg (2 metric tons)4,409 lb (2 metric tons) |
Specifications are configuration-dependent and are confirmed during engineering review of your part drawings.
Yes. Whether you are installing a Patt Rotary III, Rotary IV or Colossus system or connecting third-party extruders, melt pumps and dies, Patt designs and machines custom inlet/outlet adapters, flanges and heated crossover pipes to match your line heights, bolt patterns and bore diameters.
For corrosive condensates or frequent hydrolysis/pyrolysis cleaning, Patt offers stainless and precipitation-hardening tooling grades (PEA, PEA+ and Patt Corrosion) paired with low-temperature pulse plasma ion nitriding so the working surface resists wear, galling and scraper damage without stripping stainless corrosion resistance.
Our process
Review the polymer or part, operating conditions, drawings and production targets.
Coordinate flow geometry, material, surface treatment and the installation envelope.
Bring machining, nitriding and dimensional checks together in our Quebec facility.
Discuss installation, operation, cleaning and ongoing service with the team who built it.
Patt Technologies
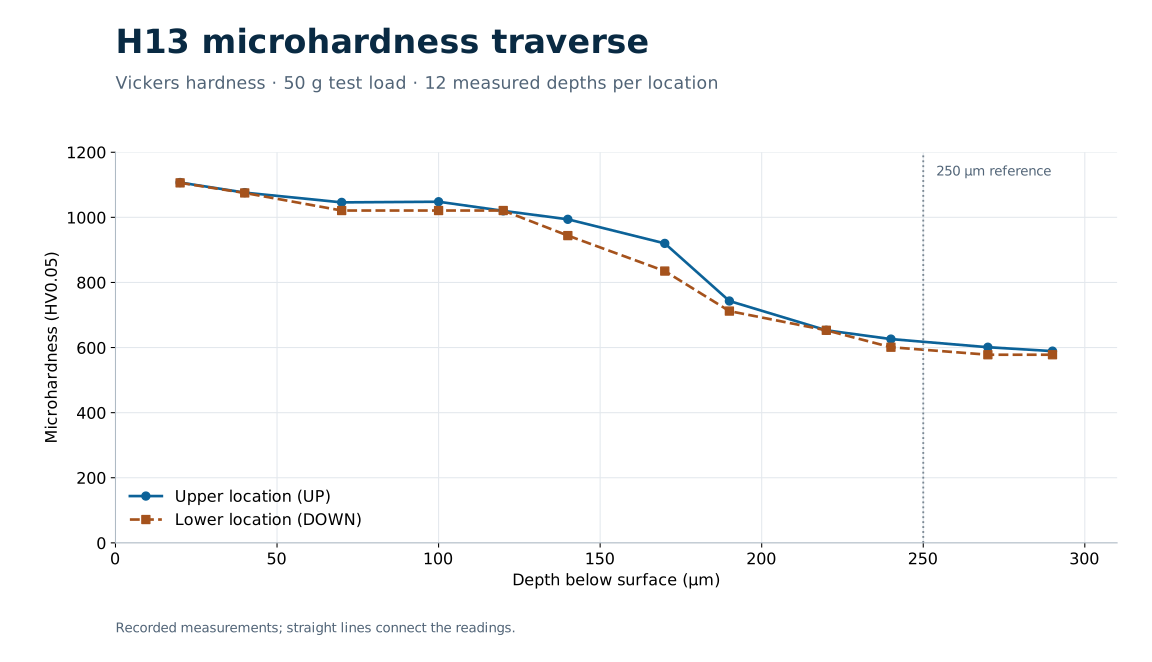
Review the micrographs and 24-point microhardness traverse from the published technical case study.
ExploreSee the geometry, installation envelope and material options behind the Patt wave upgrade.
ExploreEngineering reference
Plasma vs. gas nitriding and hard chrome for extrusion tooling · Tool steel selection
Discuss your project
Send the polymer, throughput and operating conditions, or the drawing and material requirements for your part.
sales@patt-tech.com